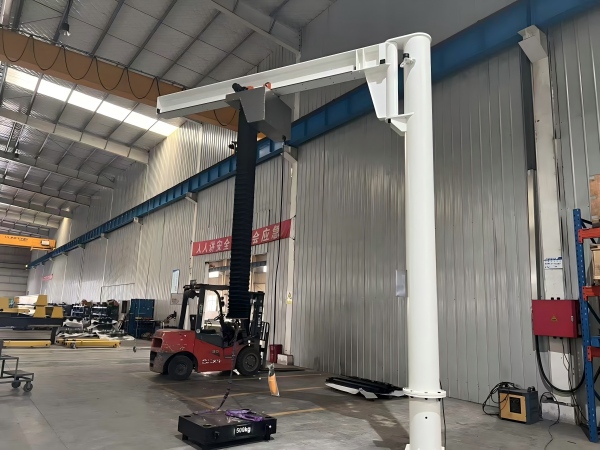
Relying on advanced cleanroom engineering and reliable product quality, we successfully delivered a 1T food-grade motorized articulated jib crane to Colombia, providing a tailor-made lifting solution for a leading food and beverage manufacturer's ISO 7 cleanroom operations.
Expanding a high-cleanliness production line requires precise engineering, a reality recently faced by a leading food and beverage manufacturer in Bogotá, Colombia. As part of their facility upgrade to meet strict hygiene demands, the plant needed to handle raw ingredients and packaging components inside an ISO Class 7 cleanroom. However, standard lifting equipment fell short due to strict particulate emission limits, tight spatial layouts, and mandatory washdown protocols. Traditional rigid-boom cranes could not maneuver around interior structural pillars without creating operational dead zones. To resolve this, we engineered and supplied a customized 1T food-grade motorized articulated jib crane. This solution delivered smooth, dead-zone-free articulation while ensuring zero particulate contamination, perfectly balancing heavy-duty capability with uncompromising cleanroom compliance.
Operating within a controlled cleanroom environment introduces severe mechanical constraints. The project encountered three distinct technical hurdles:
Particulate and Lubrication Limits (ISO Class 7 Compliance): Standard cranes use open gear systems and standard industrial greases that shed microscopic particles and emit volatile organic compounds (VOCs), violating ISO 14644-1 standards for Class 7 cleanrooms.
Rigorous Sanitary Washdown Protocols: Food-processing equipment undergoes frequent high-pressure cleaning using chemical disinfectants. Standard carbon steel structures suffer from rapid corrosion and peeling paint, which risks product contamination.
Spatial Obstructions: The production floor featured multiple structural load-bearing columns and tight machinery placement. A fixed-boom crane lacked the flexibility to reach around these barriers.
To overcome these constraints, our engineering team designed a specialized material handling solution tailored to the client's operational footprint:
Articulated Dual-Arm Architecture: The two-segment arm design allows the hoist to pivot and fold around structural columns. This geometry provides complete 360-degree coverage of the processing zone without requiring a large swinging radius.
Non-Shedding Surface Treatment: The structural steel components received a multi-layer, food-grade non-shedding epoxy coating. All exposed fasteners, pins, and critical linkage components were upgraded to 304 stainless steel to withstand daily chemical washdowns.
Cleanroom-Rated Motorized Drive: The slewing and hoisting mechanisms are driven by totally enclosed, low-noise electric motors equipped with food-grade, FDA-compliant lubricants sealed within the gearbox to prevent any possibility of leakage.
Feature | Specification |
Model | BZ-M Cleanroom Articulated Jib Crane |
Rated Capacity | 1 Ton (1000 kg) |
Arm Length / Reach | 3.5 Meters (Articulated Dual-Arm Design) |
Rotation Angle | 360° (Primary & Secondary Pivots) |
Cleanroom Class | ISO Class 7 (Fed. Std. 209E Class 10,000) |
Surface Treatment | Food-grade non-shedding epoxy coating / Stainless Steel components |
Hoist Type | Cleanroom-rated Electric Chain Hoist with food-grade lubricant |
Power Supply | 220V/440V, 3-Phase, 60Hz (Tailored for Colombian grid) |
Deploying heavy industrial machinery internationally requires meticulous alignment with regional regulations and logistics networks. The electrical system of the jib crane was fully calibrated to match Colombia's standard industrial grid (220V/440V, 60Hz). Furthermore, our supply chain and logistics partners ensured smooth customs clearance and transportation directly to the client's facility. The equipment is fully compliant with local industrial standards, with fast shipping and regional logistics support available to Bogota, Medellin, Cali, and other major industrial hubs across Colombia.
"In our beverage packaging line, maintaining strict hygiene while handling heavy ingredients is a constant balancing act. The 1T motorized articulated jib crane installed in our cleanroom has transformed our workflow. The articulated arm allows us to reach around structural pillars smoothly without generating dust or particulate matter. It met all our sanitary audit requirements seamlessly."
— Plant Operations Manager, Food & Beverage Processing Facility, Bogotá, Colombia
A: Yes. The crane is specifically engineered for ISO Class 7 environments, utilizing non-shedding materials and food-safe lubricants. Furthermore, our equipment is fully compliant with local industrial standards, with fast shipping and logistics support available to Bogota, Medellin, Cali, and other major industrial hubs across Colombia.
A: Unlike standard rigid-boom jib cranes, the articulated dual-arm design provides exceptional flexibility. It can fold and maneuver around obstacles, ensuring dead-zone-free lifting coverage inside tight processing zones.
A: Routine maintenance includes inspecting the stainless steel fasteners, checking the sealed food-grade gearbox lubrication, and verifying the integrity of the non-shedding epoxy coating during scheduled plant shutdowns.
Investing in purpose-built material handling equipment protects product integrity and minimizes operational downtime in high-cleanliness environments. If you are looking for a reliable, sanitary lifting solution tailored to your facility in Colombia or Latin America, KUNFENG offers custom-engineered jib cranes designed to meet strict international and local standards.
Contact our engineering team today for a customized quote and layout design.